Performance Enhancement of Rotating Machinery
Global mechanical sourcing, Total Cost of Ownership (TCO) optimization, and dedicated aftermarket support—delivered by a highly qualified, multilingual team of experts.
Core Technologies
Oil-Lubricated Screw and Piston Compressors:
Complete Compressed Air Systems
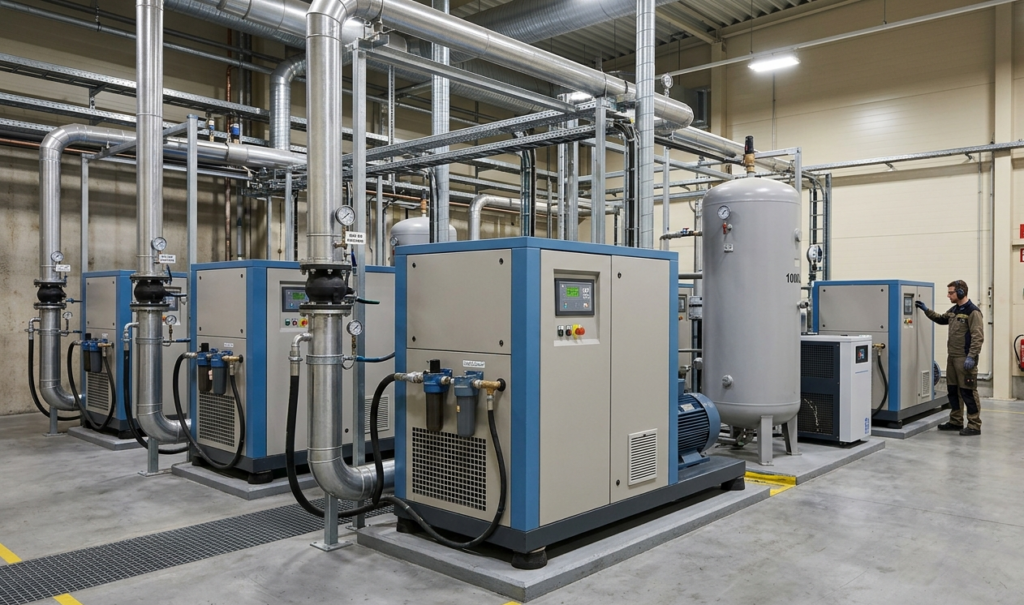
Maximize efficiency, uptime, and long-term durability with our comprehensive range of oil-lubricated rotary screw and piston compressors. Engineered to withstand the most demanding industrial environments, our screw compressors deliver a highly efficient, continuous airflow with optimized energy consumption, while our heavy-duty piston compressors offer reliable performance for high-pressure and intermittent duty cycles.
To ensure maximum process air quality and protect your downstream equipment, we offer a fully integrated air treatment portfolio, including high-performance refrigerated and desiccant dryers, precision inline filters, reliable condensate drains, and certified air receivers.
Key Features:
- Heavy-duty, certified air receiver tanks with smart condensate management.
- High-efficiency screw air ends offering minimal life-cycle costs.
- Integrated air treatment: refrigerated and desiccant dryers for optimal dew point control.
- Advanced filtration systems for precise oil and particulate removal.
Aftermarket Support
Our commitment goes far beyond the sale. We deliver uncompromising aftermarket support—offering genuine OEM spare parts, proactive maintenance programs, and 24/7 technical assistance to minimize downtime and maximize the service life of your compressed air infrastructure.
Oil-Free Rotary Screw Compressors:
100% Air Purity for Mission-Critical Applications
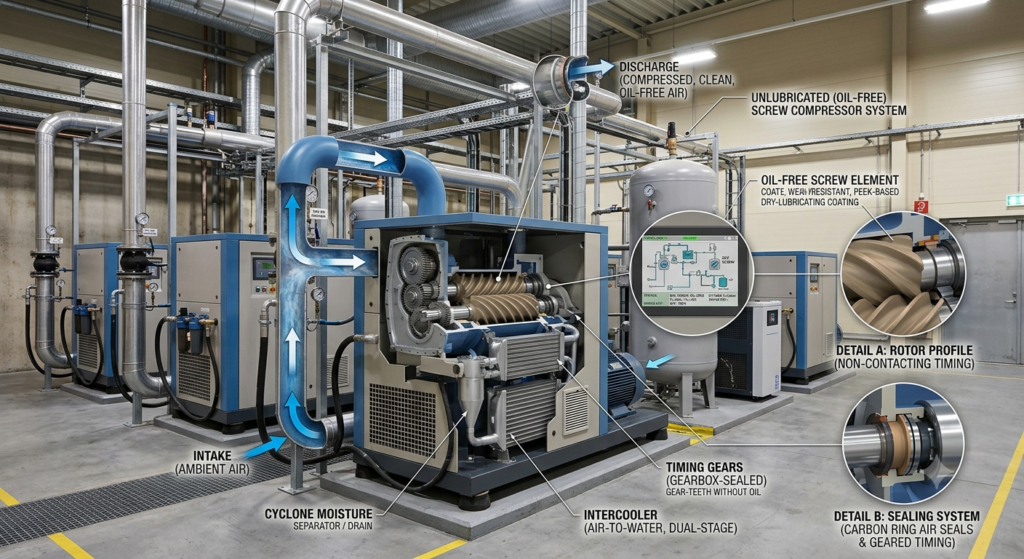
When air purity is non-negotiable, our advanced oil-free rotary screw compressors deliver absolute reliability and pristine air quality. Specifically engineered for critical sectors such as pharmaceuticals, food & beverage, electronics, and chemicals, these systems eliminate any risk of oil contamination in the production line, ensuring full compliance with the most stringent international purity standards (ISO 8573-1 Class 0).
Equipped with state-of-the-art rotor coatings, optimized cooling systems, and smart control units, our oil-free compressors ensure energy-efficient operation and smooth performance even under the most demanding workloads—safeguarding both product integrity and your brand reputation.
Key Features:
- ISO 8573-1 Class 0 certified oil-free air delivery.
- Advanced thermodynamic design featuring premium jacket-cooled screw air ends.
- Exceptional energy efficiency with Variable Speed Drive (VSD) options.
- Low maintenance requirements thanks to highly wear-resistant components.
Process Centrifugal Pumps:
API & ISO Compliant Solutions for Engineered Applications
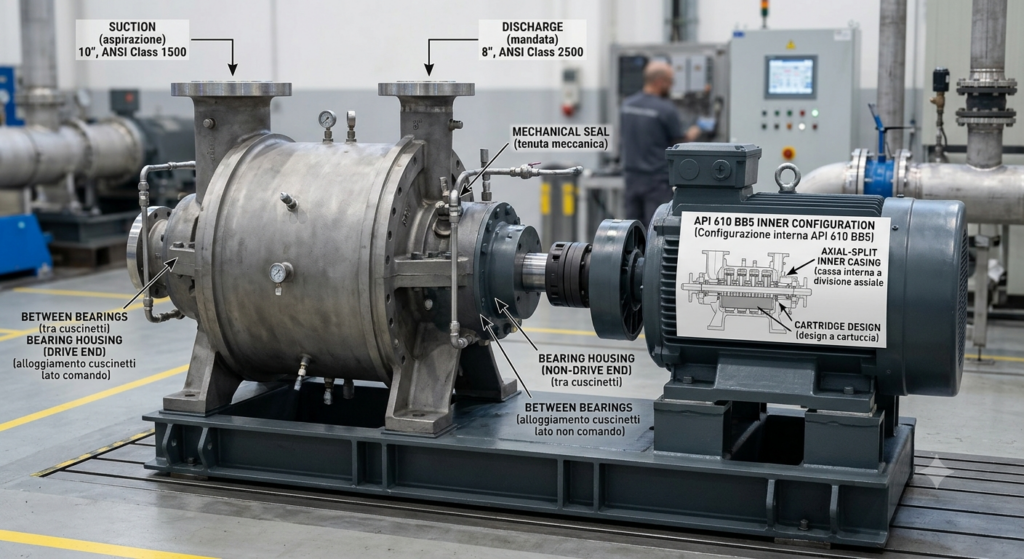
PoHigh-tech, heavy-engineered process pumps strictly compliant with international standards. Our portfolio is engineered to safely and efficiently handle corrosive, volatile, toxic, and high-temperature fluids, ensuring full compliance with demanding industry technical specifications.
Product Portfolio & Standards:
- API 610: Heavy-duty centrifugal pumps custom-designed for refinery and hydrocarbon processing services.
- API 675: Positive displacement metering pumps for ultra-high precision chemical injection.
- API 685: Sealless magnetic-drive centrifugal pumps, ensuring total leak containment for hazardous liquids.
- API 674: Reciprocating positive displacement pumps for high-pressure washing and industrial injection applications.
- ISO 5199: High-performance chemical process pumps engineered for maximum versatility and reliability in chemical plants.
Key Benefits:
Maximum operational safety and environmental protection against hazardous leaks.
Heavy-duty construction optimized for extreme pressures and temperatures.
High Mean Time Between Failures (MTBF) and fully customizable configurations.
Water & Wastewater Management
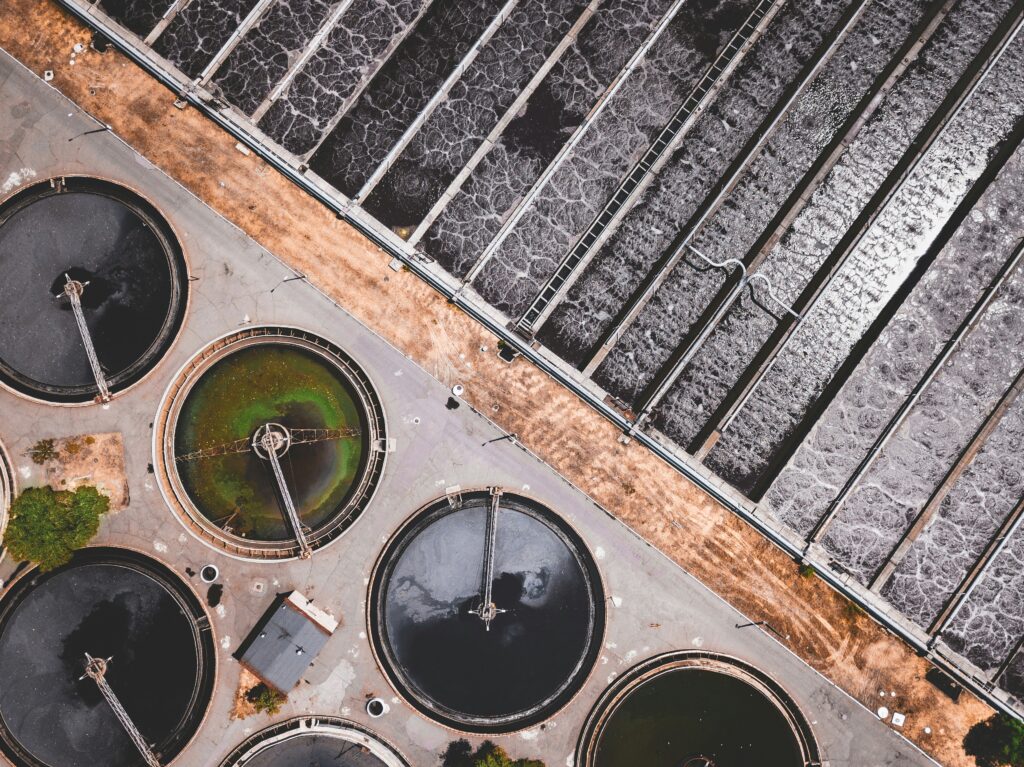
Reliable water infrastructure demands heavy-duty, high-capacity pumping solutions engineered to handle massive volumes of water and complex slurries. We offer a comprehensive lineup of pumps designed specifically for municipal waterworks, clean water distribution, and wastewater treatment facilities.
Whether handling raw sewage, industrial effluent, stormwater, or abrasive sludge, our pumps are built to prevent clogging, resist chemical corrosion, and deliver high hydraulic efficiency. From submersible wastewater pumps to high-flow split-case pumps for municipal supply, our solutions ensure seamless water cycle management and full environmental compliance.
Key Features:
- Non-clog impellers (vortex, channel, and cutter/grinder systems) for effective solids handling.
- Heavy-duty, corrosion-resistant materials (ductile iron, stainless steel, duplex).
- High-efficiency motors built for continuous, low-energy operation.
- Custom configurations for municipal, agricultural, and industrial water networks.
Mechanical Seal
Supporting Systems and Gland Packing
Preventing leaks and protecting rotating equipment is essential for maintaining plant safety and process efficiency. We offer a comprehensive range of premium fluid sealing solutions, including advanced mechanical seals and highly durable braided gland packings, engineered for pumps, agitators, mixers, and valves across all industrial sectors.
From single and dual cartridge mechanical seals for hazardous chemical containment to engineered braided packings made from cutting-edge materials (PTFE, graphite, aramid fibers), our sealing technologies are built to minimize shaft wear, reduce friction, handle extreme pressures, and withstand aggressive chemical attack.
Key Benefits:
Optimized solutions designed to minimize flush water consumption and frictional power loss.
Tailored material selection based on specific fluid, pressure, and velocity parameters.
Single, dual, and custom cartridge mechanical seals compliant with API 682 standards.
High-quality braided gland packings offering excellent thermal conductivity and chemical resistance.
High-Performance Industrial Vacuum Systems
for the Pharmaceutical and Beverage Industries
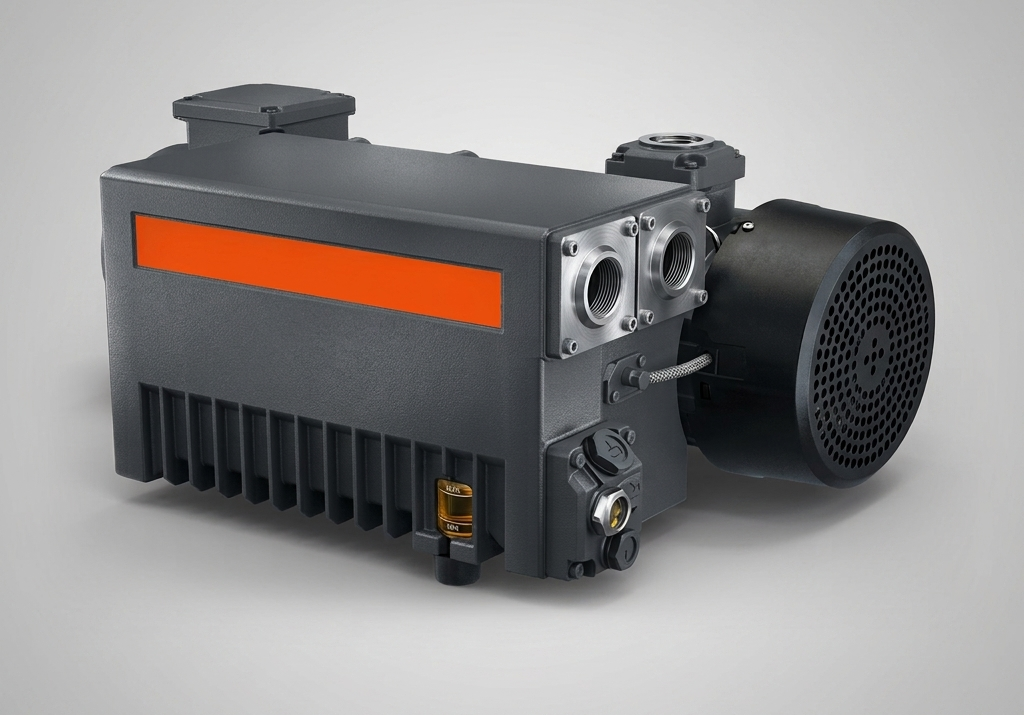
Maximize efficiency, strict hygiene, and operational uptime across your production lines with our comprehensive range of advanced industrial vacuum pumps. Engineered to meet the highest global standards for reliability and performance, our portfolio includes robust oil-lubricated rotary vane pumps, dry (oil-free) screw pumps, and contactless claw pumps. Whether handling continuous, high-volume suction for demanding process environments or managing critical intermittent duty cycles, our systems ensure optimized energy consumption and low life-cycle costs.
To safeguard process purity and protect downstream operations in highly regulated environments, we offer fully integrated vacuum systems complete with specialized inlet liquid separators, precision particulate filters, chemical-grade coatings, and sanitary-grade condensate traps (knock-out pots).
Industry-Specific Applications:
Beverage Industry
- Vacuum Filling and Bottling: Ensures fast, precise, and foam-free fill levels for glass and PET lines.
- Deaeration and Degassing: Removes dissolved oxygen from water, soft drinks, and beer prior to carbonation to extend shelf life and preserve flavor profiles.
- Pneumatic Conveying and Labeling: High-reliability pick-and-place and material handling systems for high-speed automated packaging lines.
Pharmaceutical Industry
Drying and Freeze-Drying (Lyophilization): High-vacuum performance for low-temperature freeze-drying and gentle moisture removal from sensitive active pharmaceutical ingredients (APIs).
Reactor Vacuum and Distillation: Safe extraction and processing of volatile organic compounds (VOCs) and solvents under precise, reliable pressure control.
Sterile Packaging: High-integrity vacuum sealing for blisters, vials, and pouch packaging in cleanroom environments to maintain absolute sterility.