Optimizing the Flow of Your Static Equipment
From strategic procurement to lifecycle optimization: our multilingual engineering and expert team reduces costs while ensuring the reliability of your process plants.
Technologies We Serve
High-Performance Column Internals for Distillation,
Fractionation & Mass Transfer
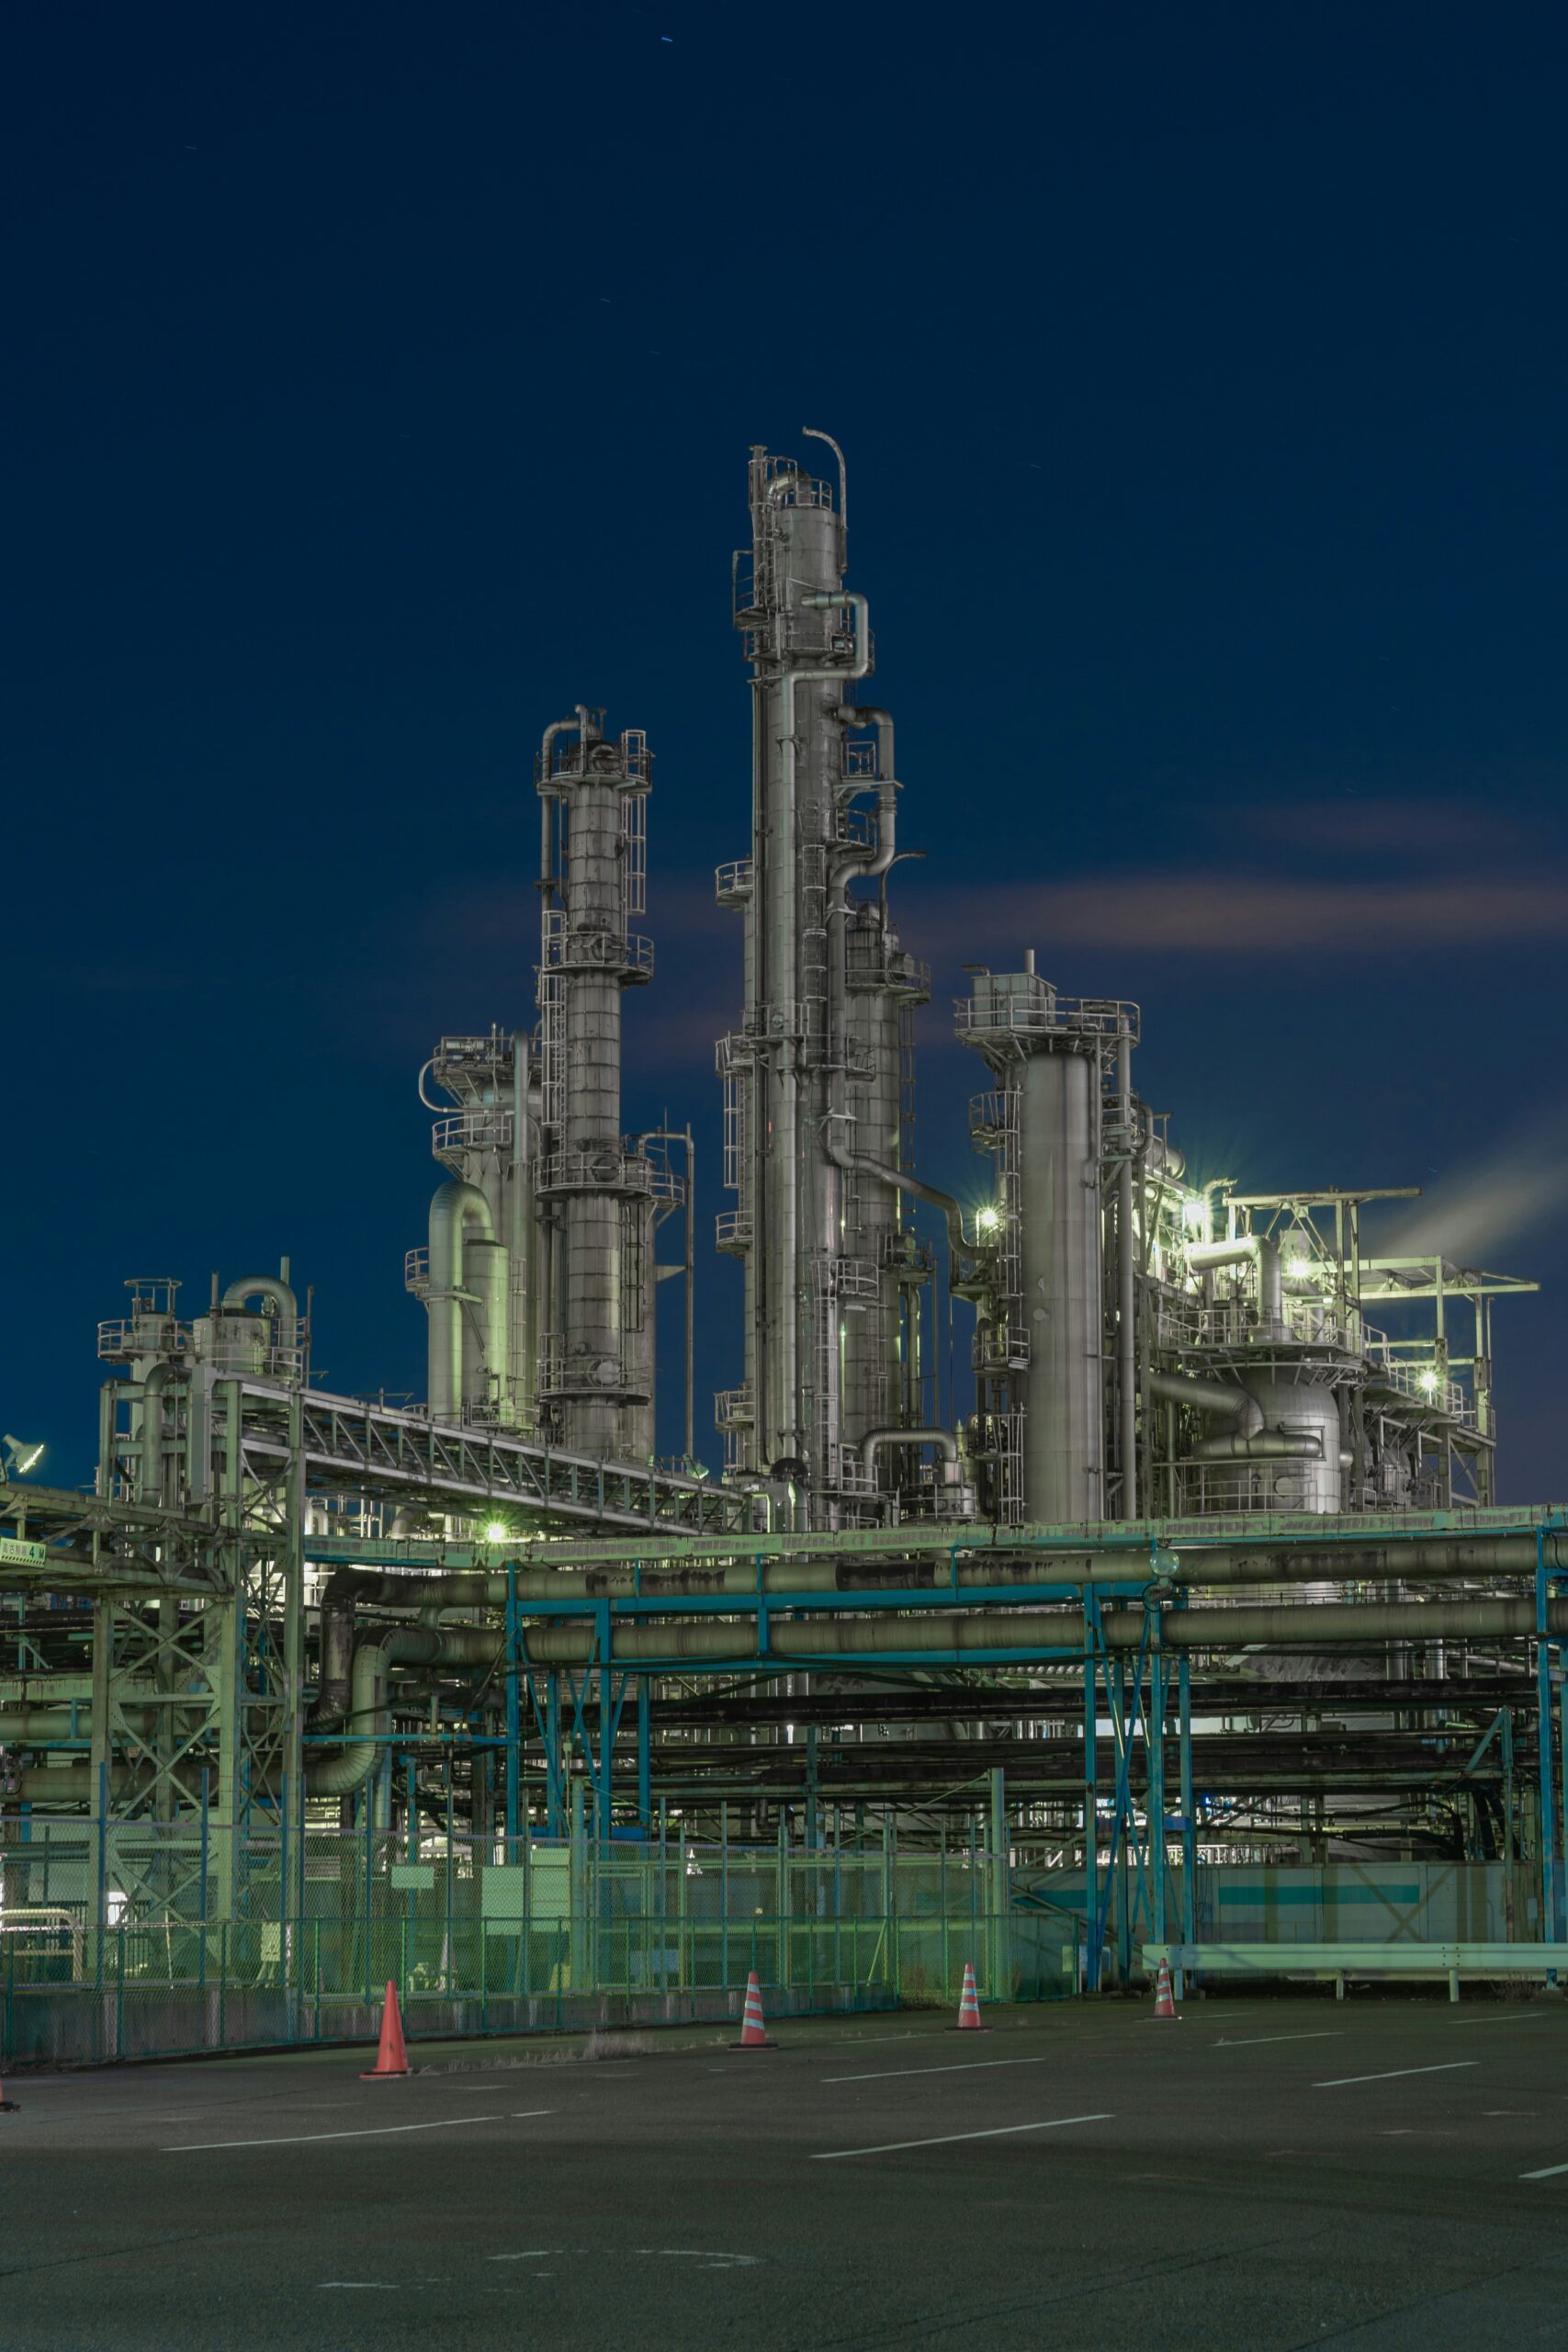
Maximize separation efficiency, throughput, and product purity with our advanced range of column internals. Engineered to optimize mass and heat transfer in the most demanding distillation, absorption, stripping, and fractionation processes, our solutions serve critical roles across the chemical, petrochemical, and refining industries. Whether you are retrofitting existing columns to boost capacity or designing a new process unit, our custom-tailored internals minimize pressure drop, prevent fouling, and enhance overall operational flexibility under varying hydraulic loads.
Product Range & Technical Highlights:
Structured & Random Packings: Premium high-surface-area solutions designed to optimize liquid-gas contact while maintaining ultra-low pressure drops.
Mass Transfer Trays: A complete selection of sieve, valve, and bubble-cap trays engineered for wide operating ranges and reliable hydraulic performance.
High-Precision Liquid Distributors: Custom-designed gravimetric and pressurized distributors ensuring uniform liquid allocation across the packing bed to eliminate channeling.
Phase Separators & Support Internals: Robust support grids, bed limiters, and high-efficiency mist eliminators (demisters) for clean phase separation.
High-Efficiency Inline Static Mixers for Continuous Processing
Achieve perfect fluid homogeneity with zero moving parts. Our advanced inline static mixers utilize a series of precisely engineered geometric elements to induce controlled radial mixing, blending fluids seamlessly directly within your pipeline. Designed for both laminar and turbulent flow regimes, these motionless mixers offer a highly reliable, low-maintenance, and energy-efficient alternative to dynamic agitation systems. They are widely utilized across water treatment, chemical processing, oil & gas, and refining for continuous dosing, pH adjustment, gas-liquid dispersion, and multi-viscosity blending operations.
Key Advantages:
Maintenance-Free Operation: No moving parts means zero mechanical wear, zero lubrication requirements, and dramatically reduced operational downtime.
Low Pressure Drop & High Energy Savings: Optimized geometric designs maximize mixing intensity while conserving valuable process line pressure.
Versatile Configurations: Available in a wide variety of materials (stainless steel, duplex, exotic alloys, and high-performance plastics) and element types (helical, cross-flow, V-shaped) tailored to your specific process viscosity and chemical compatibility.
Compact Inline Design: Space-saving footprint that integrates seamlessly into existing piping networks without requiring extensive structural modification.
Industrial Heat Exchangers:
Advanced Thermal Management Solutions
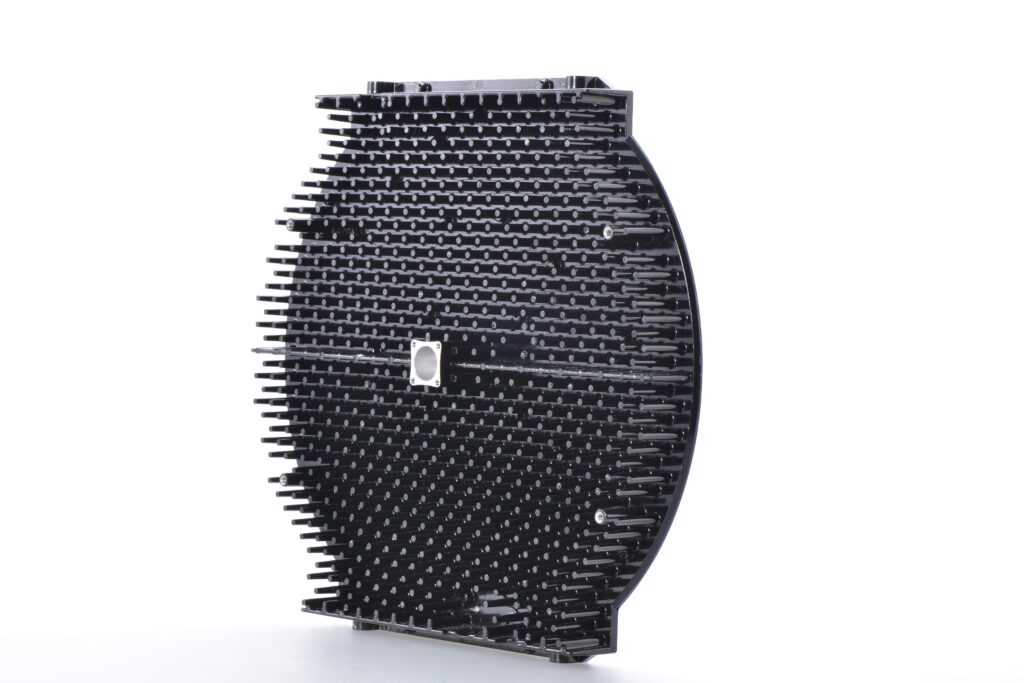
Optimize thermal efficiency and maximize energy recovery across your plant with our comprehensive portfolio of industrial heat exchangers. Engineered to withstand high temperatures, extreme pressures, and highly corrosive fluids, our thermal management systems are built for maximum heat transfer coefficients and long-term mechanical integrity. From standard industrial utility applications to custom-engineered process units compliant with international codes (such as ASME and TEMA standards), we provide the ideal configuration to minimize fouling, reduce your energy footprint, and ensure reliable continuous operation.
Product Range & Technical Highlights:
Shell and Tube Heat Exchangers: Robust, heavy-duty configurations ideal for high-pressure, high-temperature, and severe-duty process services in refineries and chemical plants.
Plate Heat Exchangers (Gasketed, Welded, & Brazed): Ultra-compact solutions delivering exceptional thermal efficiency with minimal footprints, optimized for easy maintenance access and cleaning.
Air-Cooled Heat Exchangers (Fin-Fan Coolers): Engineered for heavy industrial cooling applications, particularly in water-scarce environments.
Premium Material Selection: Available in carbon steel, stainless steel, duplex, titanium, and exotic alloys to withstand highly aggressive, abrasive, or acid-containing process media.